Attempt 1: With an initial value of G2=680 mbar, cryocleaning commenced, immediately raising G2=983 mbar (G1=648 mbar). G1 dropped to 555 mbar when V12A is closed. When V12A is opened again, G1 goes up to 649 mbar and remains there, suggesting a possible block between coldtrap 1 and 13A. Pump back to dump.
Attempt 2: Before commencing cryocleaning: G1=0.4 mbar, G2= 677 mbar, P1=0.014 mbar. Once cleaning has been initiated, G1=646 mbar, G2= 982 mbar, P1= 1000 mbar. Close V14, resulting in G1=698 mbar, G2=638 mbar and P1=0.016 mbar. This seems to indicate that some mixture in G2 flowed through the safety valve into the dump and thus raised G1. Still no indication of pump affecting region of fridge after the cold trap. Pump back to dump.
Attempt 3: The purpose of this attempt was to try reducing the percent by which V6 is open, hopefully reducing the flow of mixture to the pump. Initially G1=0.7 mbar, G2=674 mbar, P1=0.014 mbar. Opening V4 results in G1=685 mbar, G2=674. Opening V14 resulted in a sudden flow of G1=581 mbar and G2=982 mbar. Note that V6 is still closed and thus there should be no mixture flowing to G2. This is a huge indicator that V6 is malfunctioning. This is further suggested by pumping to the dump, which can be done with V6 “closed”, since mixture is freely passing through the valve.
Attempt 4: This test is performed to verify that V6 is working improperly. Initially G1=17 mbar, G2=674 mbar, P1=0.02 mbar. Opening V4 (V12A open) results in G1=696 mbar, G2=674 mbar. Opening V13A results in G1=692 mbar, G2=629 mbar. These values seemed stable, possibly indicating that mixture is not being pumped into the dump? Opening V14 (with V6 closed) resulted in G1=635 mbar and G2=982 mbar. The results of attempt 3 have been repeated. The issue (or at least one issue), is due to V6 malfunctioning.
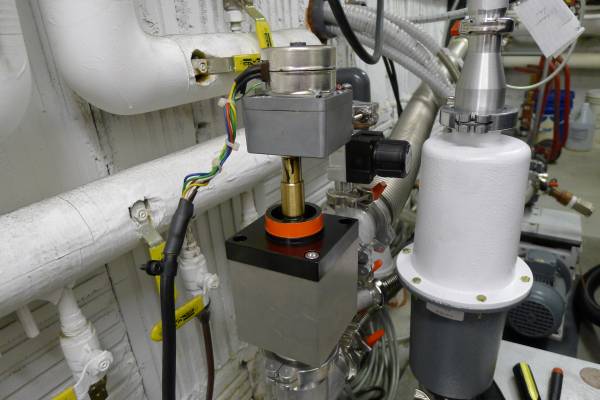
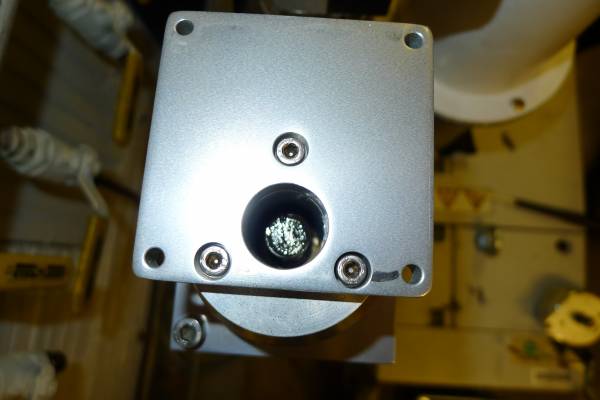
The issue with V6 has occurred before and is due to a screw inside the motorized part of the valve. To deal with this issue we opened up the motorized portion of V6 and found the screw. Pictures included below.